

What is a diatomaceous earth mineral powder pneumatic conveyor? What is its design principle?
For industries dealing with fine powders like diatomaceous earth, efficient material handling is crucial. A pneumatic conveyor, specifically designed for diatomaceous earth mineral powders, offers a solution that combines reliability with advanced engineering. This article explores the functionality of such equipment, focusing on its design principles and how it addresses the unique challenges of transporting diatomaceous earth. By understanding the core mechanics and design considerations, users can appreciate the importance of specialized equipment in maintaining operational efficiency and product quality.

HeadPowder: A Leader in Pneumatic Conveyor Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in developing and manufacturing advanced pneumatic conveying systems tailored to the needs of various industries. Our company, commonly known as HeadPowder, has established itself as a trusted provider of high-quality equipment for mineral powder handling. With a strong commitment to innovation and customer satisfaction, HeadPowder offers solutions that enhance productivity and ensure the safe and efficient transport of materials. Our headquarters are located in Shandong, China, where our team of experts continuously researches and improves conveyor technologies to meet evolving industry demands.
The Design Principles of Diatomaceous Earth Pneumatic Conveyors
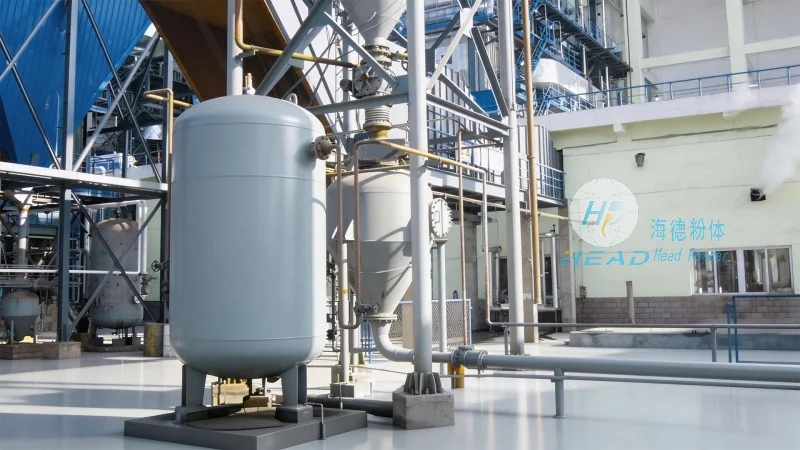
The design of a diatomaceous earth mineral powder pneumatic conveyor is built on several key principles that ensure optimal performance. First, the system must handle the specific properties of diatomaceous earth, which includes its fine particle size and low bulk density. These characteristics require specialized components to prevent clogging and ensure consistent flow. The design incorporates high-efficiency air pumps and ductwork that can handle the low pressure and high volume requirements of fine powders. Additionally, the system is engineered with materials that resist abrasion and corrosion, as diatomaceous earth can be abrasive over time. The control systems are designed to monitor and adjust air pressure and flow rates in real-time, allowing for precise control and minimizing material loss. This combination of engineering features ensures that the conveyor operates efficiently while maintaining the integrity of the diatomaceous earth powder.
Key Components and Their Roles
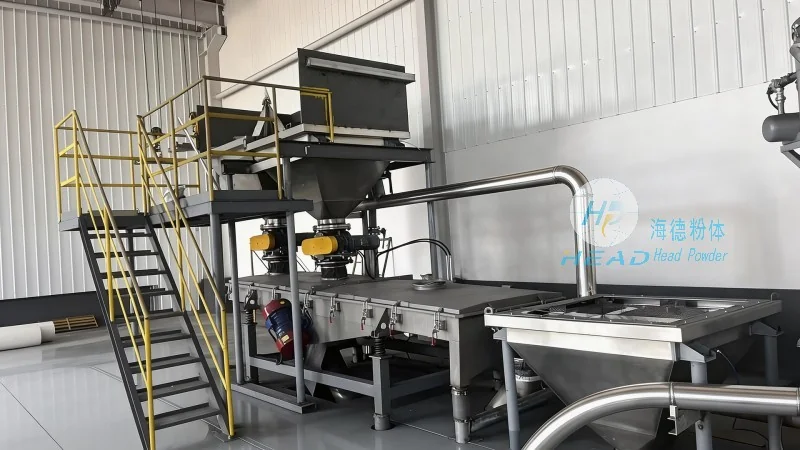
Several critical components make up a diatomaceous earth pneumatic conveyor. The air compressor is the heart of the system, providing the necessary pressure to move the powder through the ducts. The hopper or feeder is designed to hold the diatomaceous earth and feed it into the system at a controlled rate. The ductwork, often made of stainless steel or other corrosion-resistant materials, carries the powder and air mixture. The separation or cyclone unit is crucial for separating the powder from the air, allowing the powder to be collected and the air to be recycled. Each component is carefully selected and integrated to work in harmony, ensuring smooth operation and minimal downtime. The design also includes safety features such as pressure relief valves and overfill protection to prevent accidents and protect the equipment.
Benefits of Using a Specialized Pneumatic Conveyor for Diatomaceous Earth
Implementing a diatomaceous earth pneumatic conveyor offers numerous benefits for industrial operations. One of the primary advantages is the ability to transport the powder in a closed system, which prevents contamination from external sources and minimizes dust emissions. This is particularly important for diatomaceous earth, which is often used in food and pharmaceutical applications where purity is paramount. The closed system also reduces the risk of product loss and improves overall material recovery rates. Additionally, pneumatic conveyors are generally more flexible than traditional belt or screw conveyors, allowing for changes in the layout or direction of the material flow. This flexibility makes them ideal for complex production lines where multiple destinations are required. The energy efficiency of pneumatic conveyors, especially when compared to other bulk material handling methods, also contributes to lower operational costs over time. By investing in a specialized conveyor, businesses can enhance their operational efficiency, improve product quality, and reduce environmental impact.

Conclusion and Company Commitment
In conclusion, a diatomaceous earth mineral powder pneumatic conveyor is a sophisticated piece of equipment that leverages advanced design principles to handle the unique challenges of transporting fine powders. The system’s ability to maintain product integrity, operate efficiently, and adapt to various industrial needs makes it an essential component for many industries. Shandong HeadPowder Engineering Co., Ltd., as a leading manufacturer in this field, continues to innovate and provide high-quality solutions that meet the evolving demands of the market. With our headquarters in Shandong, China, we remain committed to delivering reliable and effective pneumatic conveyor systems that help our clients achieve their operational goals while maintaining the highest standards of safety and performance.