

Principle and Working Scene Characteristics of Rice Husk Ash Powder Conveying System
The rice husk ash powder conveying system is a specialized equipment designed for the efficient transportation of rice husk ash powder, a byproduct from the rice processing industry. This system is crucial for industries that rely on rice husk ash as a raw material or for waste management purposes. The system operates based on principles of pneumatic conveying, utilizing air to move the fine powder through pipelines with precision and control.

Working Principle of the Powder Conveying System
The core of the rice husk ash powder conveying system lies in its pneumatic conveying mechanism. The system typically consists of a hopper for material storage, a blower or air compressor to generate the necessary airflow, and a pipeline network to transport the powder. The process begins with the rice husk ash being fed into the hopper. The blower then creates a low-pressure zone in the pipeline, which draws the powder into the air stream. As the powder is carried by the air, it moves through the pipeline to the destination point, such as a storage silo or processing unit. The system may include components like rotary valves, filters, and pressure regulators to ensure smooth operation and prevent blockages or dust emissions.
Key Components and Their Functions
Several key components work in tandem to ensure the efficient operation of the rice husk ash powder conveying system. The hopper serves as the initial storage and feeding unit, providing a controlled supply of the powder. The blower or air compressor is responsible for generating the airflow that propels the powder. The pipeline network, often made of stainless steel or other corrosion-resistant materials, is designed to handle the fine particles without clogging. Rotary valves are used at the inlet and outlet to control the flow of material, preventing backflow and ensuring a steady supply. Filters are integrated to capture any fine particles that might escape, maintaining air quality and preventing contamination. Pressure regulators help maintain consistent airflow pressure, optimizing the conveying efficiency.
Working Scene Characteristics and Applications
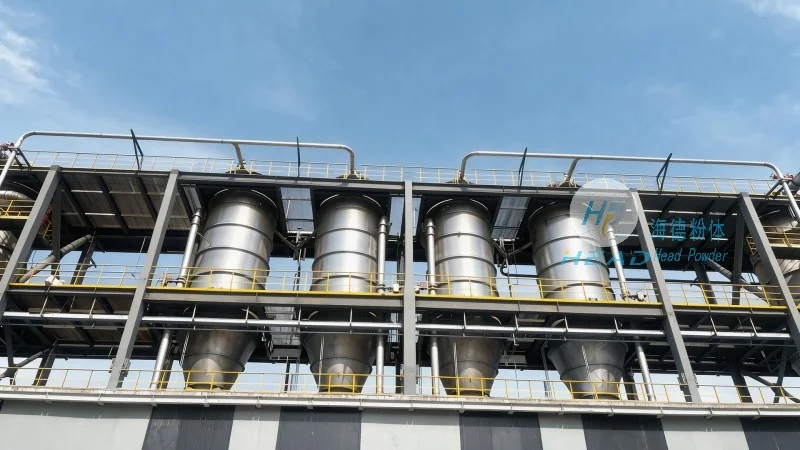
The rice husk ash powder conveying system is widely used in various industrial settings, particularly in the agricultural and chemical sectors. Its working scene characteristics are tailored to handle the specific properties of rice husk ash, which is a fine, light powder with a tendency to agglomerate. The system is designed to handle these challenges by ensuring proper air flow and particle separation. In industrial applications, this system is used for transporting rice husk ash from storage areas to processing plants, or from processing units to storage silos. It is also utilized in waste management facilities where rice husk ash is a byproduct of rice husk combustion. The system's ability to handle large volumes of powder efficiently makes it suitable for high-capacity operations, such as in large-scale rice processing plants or biomass energy facilities.

Advantages of the Powder Conveying System
Implementing a rice husk ash powder conveying system offers several advantages for industrial operations. Firstly, it provides a dust-free and clean conveying method, which is essential for maintaining a safe working environment and complying with environmental regulations. Unlike traditional methods like bucket elevators or belt conveyors, pneumatic conveying minimizes dust generation and reduces the risk of inhalation by workers. Secondly, the system offers high efficiency in terms of material transport, as it can handle large volumes of powder with minimal energy consumption. The use of air as the conveying medium allows for a compact design, reducing the footprint of the system in industrial facilities. Additionally, the system is versatile and can be adapted to different production scales, from small-scale operations to large industrial plants. It also reduces labor costs by automating the material handling process, as the system can operate continuously without the need for manual intervention.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in powder handling and conveying systems. The company is headquartered in Shandong, China, and has established itself as a trusted provider of industrial equipment for various industries. With a focus on innovation and quality, headpowder develops and manufactures advanced powder conveying systems tailored to the specific needs of its clients. The company's products are designed to meet international standards and are known for their durability, efficiency, and reliability. Headpowder's team of engineers and technicians work closely with clients to understand their operational requirements and provide customized solutions that enhance productivity and safety. The company's commitment to customer satisfaction and technological advancement has made it a preferred choice for businesses seeking reliable powder handling solutions.