

What is a Tonne Bag Broken Bag Material Handling and Conveying System? Exploring Its Design Principl
Understanding the Tonne Bag Broken Bag Material Conveying System: Design Principles and Functionalities

Introduction to Tonne Bag Broken Bag Material Handling Systems
The Tonne Bag Broken Bag Material Conveying System is a specialized industrial equipment designed to handle and transport bulk materials that are delivered in large tonne bags, which may have been damaged or broken during handling or storage. This system is crucial in various industries such as mining, construction, agriculture, and chemical processing, where efficient material handling is essential for maintaining productivity and reducing operational costs. The system integrates multiple components to ensure safe, reliable, and efficient material transfer from the point of arrival to the processing or storage area.
Key Components and Functionalities of the System
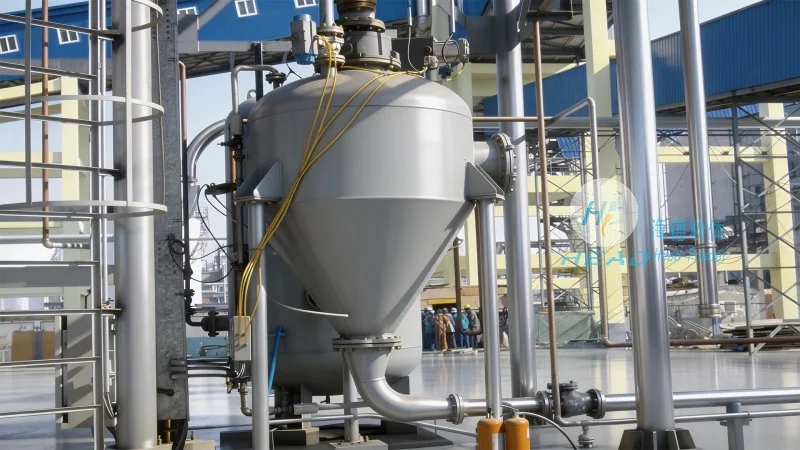
At the core of the Tonne Bag Broken Bag Material Conveying System are several key components that work in tandem to achieve seamless material handling. The primary components include a broken bag opening mechanism, a material extraction unit, a conveyor system, and a dust control system. The broken bag opening mechanism is engineered to safely open damaged or torn tonne bags without causing further damage to the material inside. This mechanism typically uses hydraulic or mechanical force to cut or tear the bag open, allowing the bulk material to flow out. The material extraction unit then collects the discharged material and directs it into the conveyor system. The conveyor system, which may consist of belt conveyors, screw conveyors, or pneumatic conveyors depending on the material characteristics and application requirements, transports the material to the next processing stage. The dust control system is integrated to manage and minimize dust generation during the material handling process, ensuring a safe and clean working environment.

Design Principles Behind the System
The design of the Tonne Bag Broken Bag Material Conveying System is guided by several fundamental principles aimed at optimizing performance, safety, and efficiency. One of the key design principles is modularity, which allows the system to be customized and adapted to different material types, bag sizes, and operational requirements. This modularity ensures that the system can be easily scaled or modified as production needs change. Another important principle is durability and robustness, as the system is designed to withstand the harsh conditions of industrial environments, including heavy loads, abrasive materials, and frequent operation. The system is constructed using high-quality materials such as stainless steel, alloy steel, and wear-resistant components to ensure long service life and minimal maintenance. Additionally, the design emphasizes safety, incorporating features like emergency stop buttons, safety guards, and material flow monitoring to prevent accidents and ensure operator safety. The system also prioritizes energy efficiency, using advanced motor controls and energy recovery mechanisms to reduce power consumption and operational costs.

Applications and Benefits in Industrial Settings
The Tonne Bag Broken Bag Material Conveying System finds wide applications in various industrial sectors where bulk material handling is critical. In the mining industry, it is used to process ore and mineral concentrates delivered in tonne bags, facilitating efficient ore processing and transportation. In the construction industry, it helps in handling cement, sand, and other building materials, ensuring smooth supply to construction sites. In the agricultural sector, it is employed for handling fertilizers, seeds, and other agricultural products, supporting efficient farming operations. In the chemical processing industry, it aids in handling raw materials and intermediates, contributing to streamlined production processes. The benefits of using this system include increased productivity due to faster material handling, reduced labor costs as manual handling is minimized, lower material loss and contamination due to efficient processing, and improved safety in the workplace. Furthermore, the system helps in maintaining a clean and organized work environment by controlling dust and managing material flow effectively.
Customization and Integration with Existing Systems
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized Tonne Bag Broken Bag Material Conveying Systems tailored to the specific needs of clients. The company, known as HeadPowder, offers a range of solutions that can be integrated with existing industrial systems, such as batching plants, storage silos, and processing equipment. Customization options include different conveyor types, bag opening mechanisms, and control systems to match the client's operational requirements. The company's engineering team works closely with clients to understand their material characteristics, handling volumes, and operational constraints, ensuring that the final system meets all performance and safety standards. HeadPowder also provides after-sales support, including maintenance services, spare parts supply, and technical assistance, to ensure the long-term reliability and efficiency of the system.
Conclusion: The Importance of Advanced Material Handling Solutions
In conclusion, the Tonne Bag Broken Bag Material Conveying System is a vital piece of industrial equipment that plays a crucial role in modern material handling operations. Its design, based on principles of modularity, durability, and safety, ensures efficient and reliable performance in various industrial applications. By integrating advanced components and control systems, this system helps industries improve productivity, reduce costs, and enhance workplace safety. As material handling demands continue to evolve, the Tonne Bag Broken Bag Material Conveying System remains a key solution for businesses seeking to optimize their material handling processes and stay competitive in the market.