

Working Principle and Features of Tonne Bag Unloading Material Conveying Systems
For industrial facilities handling bulk materials, efficient and reliable material handling solutions are crucial to maintaining operational efficiency and reducing downtime. Tonne bag unloading material conveying systems represent a sophisticated approach to managing the flow of bulk materials from large, heavy-duty bags into processing or storage systems. This article explores the working principle and key features of such systems, highlighting how they enhance material handling processes in various industrial applications.

Introduction to Tonne Bag Unloading Material Conveying Systems
A tonne bag unloading material conveying system is a specialized piece of equipment designed to automate the process of extracting bulk materials from large, heavy-duty bags and transporting them to subsequent processing or storage stages. These systems are commonly used in industries such as mining, construction, agriculture, and chemical processing, where large volumes of bulk materials need to be handled safely and efficiently. The system typically integrates several components, including a bag opening mechanism, a discharge hopper, and a conveyor system, to ensure seamless material transfer.
Working Principle of the Tonne Bag Unloading System
The operation of a tonne bag unloading material conveying system involves a series of coordinated steps to ensure the safe and efficient extraction of materials from the bags. The process begins with the placement of a tonne bag onto a designated loading platform or hopper. The system then uses mechanical or pneumatic mechanisms to open the bag, allowing the bulk material to flow into a discharge hopper. From there, the material is transferred to a conveyor system, which transports it to the desired destination, such as a storage silo, processing unit, or packaging line. The entire process is automated, minimizing manual intervention and reducing the risk of material spillage or contamination.
Key Features of the Tonne Bag Unloading Material Conveying System
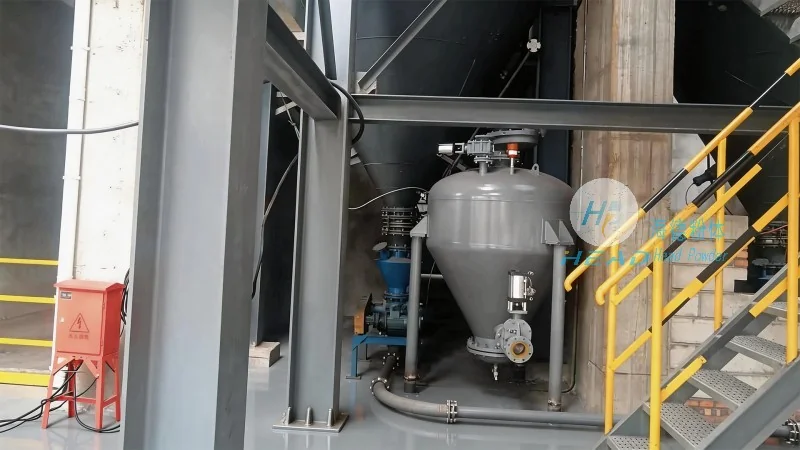
HeadPowder, a leading manufacturer of material handling solutions, offers tonne bag unloading material conveying systems with several key features that enhance performance and reliability. One of the primary features is the robust bag opening mechanism, which can handle various bag types and sizes, including woven polypropylene and plastic bags. The system is equipped with a heavy-duty discharge hopper designed to accommodate large volumes of material, ensuring consistent flow rates. Additionally, the conveyor system is engineered for high-capacity material transport, with adjustable speed and direction controls to match the specific requirements of different applications. The system also incorporates safety features, such as emergency stop buttons and overload protection, to ensure operator safety and prevent equipment damage.

Application Scenarios and Advantages
Tonne bag unloading material conveying systems are particularly beneficial in applications where large quantities of bulk materials need to be handled quickly and safely. For example, in mining operations, these systems can efficiently transfer ore from bags to crushing or grinding equipment, improving production throughput. In the construction industry, they can handle bulk materials like sand, gravel, and cement, reducing manual labor and minimizing material loss. The advantages of using such systems include increased operational efficiency, reduced labor costs, improved material handling safety, and lower maintenance requirements. By automating the material unloading process, facilities can achieve higher productivity and better control over their material flow.

Technical Specifications and Customization Options
HeadPowder provides tonne bag unloading material conveying systems with customizable options to meet the specific needs of different industrial applications. The systems are available in various sizes and configurations, with adjustable conveyor lengths and widths to accommodate different bag sizes and material volumes. The equipment is also designed for easy maintenance, with accessible components and user-friendly controls. Additionally, the systems can be integrated with other material handling equipment, such as silos or processing units, to create a comprehensive material handling solution. HeadPowder's commitment to quality and innovation ensures that their systems are built to last, providing reliable performance over the long term.
Conclusion
Tonne bag unloading material conveying systems are an essential component of modern industrial material handling, offering efficient, reliable, and safe solutions for handling bulk materials. With its robust design and advanced features, the system from HeadPowder, Shandong HeadPowder Engineering Co., Ltd., provides an effective solution for various industrial applications. By understanding the working principle and key features of these systems, industrial facilities can make informed decisions to enhance their material handling processes and improve overall operational efficiency.