

Operation Process and Working Principle of Tonne Bag Quantitative Feeding Powder Material Handling S
HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and integration of advanced material handling systems. The company is headquartered in Shandong, China, and has established itself as a trusted partner for industries requiring efficient and reliable powder processing solutions.
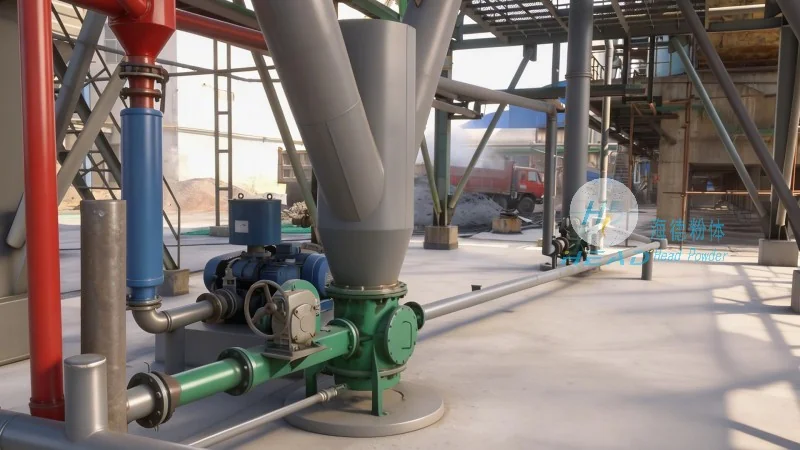
Introduction to the Tonne Bag Quantitative Feeding System
The tonne bag quantitative feeding system is a sophisticated piece of equipment engineered to handle bulk powders with precision and efficiency. This system is particularly suited for applications where large quantities of powder need to be transferred and dosed accurately, such as in chemical, pharmaceutical, food, and agricultural sectors. The system's design ensures minimal product loss, consistent flow rates, and enhanced safety during operation.
Key Components and Their Roles
The tonne bag quantitative feeding system comprises several critical components that work in tandem to achieve accurate material handling. These include the tonne bag discharging unit, a rotary valve or feeder, a hopper for material storage, and a control system for precise dosing. Each component is carefully selected and integrated to ensure optimal performance and reliability.

Operation Process of the System
The operation of the tonne bag quantitative feeding system begins with the placement of a tonne bag (also known as a super sack or big bag) onto the discharge unit. The system then uses a mechanical or hydraulic mechanism to open the bag and allow the powder to flow into the hopper. The rotary valve or feeder then regulates the flow of powder from the hopper into the downstream process equipment, such as a mixer, reactor, or packaging machine. The control system monitors the flow rate and adjusts the valve position to maintain the desired feed rate, ensuring that the material is delivered in precise quantities.

Working Principle of the System
The working principle of the tonne bag quantitative feeding system is based on the principles of gravity and controlled flow. The system utilizes a hopper with a controlled outlet, often equipped with a rotary valve or a vibratory feeder, to regulate the flow of powder. The control system uses sensors and feedback mechanisms to monitor the flow rate and adjust the valve opening to maintain the set dosage. This closed-loop control ensures that the system operates with high accuracy and repeatability, minimizing variations in the feed rate and ensuring consistent product quality.
Advantages and Applications
The tonne bag quantitative feeding system offers several advantages over traditional methods of powder handling. These include reduced labor costs, improved safety by minimizing manual handling, and enhanced accuracy in material dosing. The system is widely used in industries where precise control of powder flow is critical, such as in the production of pharmaceuticals, where dosage accuracy is paramount, or in the manufacturing of food products, where consistency is essential. Additionally, the system's ability to handle large quantities of material efficiently makes it suitable for bulk processing applications.