

What is a Barley Pneumatic Conveying System? And What Are Its Design Principles?
Barley pneumatic conveying systems are essential equipment in the grain processing industry, designed to efficiently transport barley from one location to another. These systems utilize air pressure to move the grain, offering a reliable and efficient method for handling bulk materials. The design principles behind these systems are crucial for ensuring optimal performance, safety, and durability in agricultural and food processing applications.

Understanding the Core Components of a Barley Pneumatic Conveying System
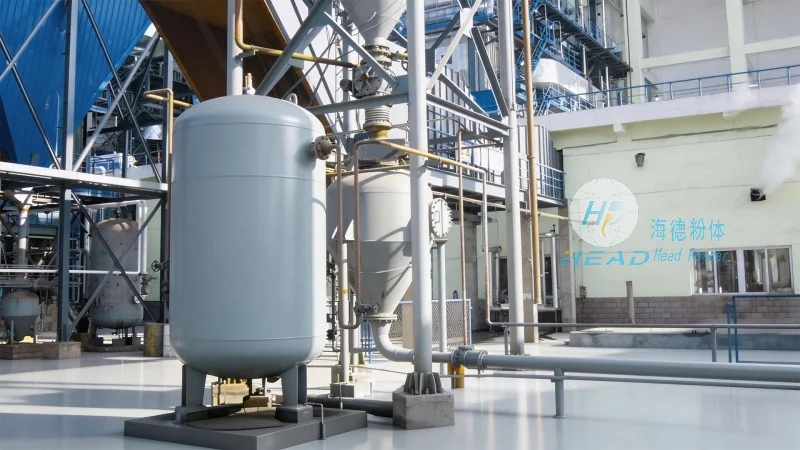
A typical barley pneumatic conveying system consists of several key components that work together to facilitate the movement of barley. The main parts include a hopper for storing the grain, a conveying line (either positive or negative pressure), a dust collector to manage airborne particles, and a discharge point for the processed barley. Each component plays a vital role in the overall functionality of the system, ensuring that the barley is transported without damage and with minimal loss.
Design Principles for Efficient Barley Handling
The design of a barley pneumatic conveying system is based on several fundamental principles to maximize efficiency and minimize operational issues. One of the primary principles is the selection of the appropriate air velocity and pressure. The air velocity must be high enough to overcome the resistance of the grain but not so high that it causes excessive wear on the system components or leads to grain breakage. The pressure system, whether positive or negative, is also carefully chosen based on the distance and height the barley needs to be transported. Additionally, the system's design considers the grain's characteristics, such as its moisture content and bulk density, to ensure that the conveying process is optimized for the specific type of barley being handled.
HeadPowder Engineering's Expertise in Pneumatic Conveying Solutions
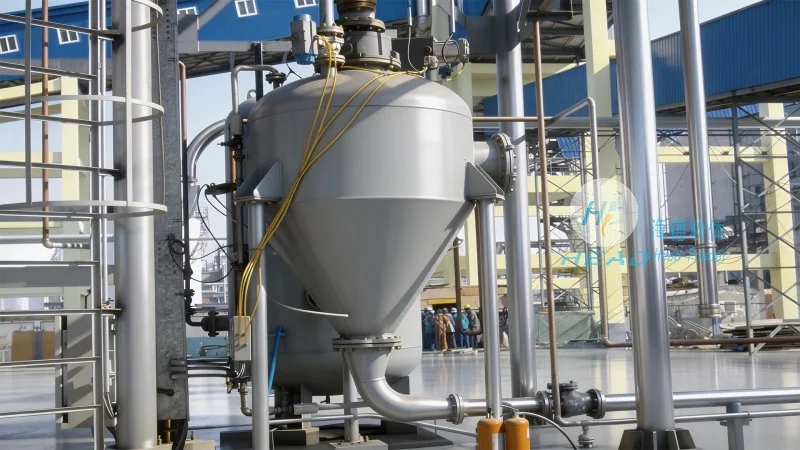
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality barley pneumatic conveying systems. With years of experience in the grain processing industry, HeadPowder has developed advanced systems that meet the stringent requirements of modern agricultural operations. The company's engineers utilize cutting-edge technology and rigorous testing to ensure that each system is tailored to the specific needs of their clients, whether for small-scale or large-scale barley processing facilities. HeadPowder's commitment to quality and customer satisfaction has made them a trusted partner for businesses seeking reliable and efficient pneumatic conveying solutions.
Key Features and Benefits of Barley Pneumatic Conveying Systems
Barley pneumatic conveying systems offer numerous benefits that make them a preferred choice for many grain processors. One of the main advantages is the ability to transport barley over long distances and vertical heights without the need for complex machinery or extensive infrastructure. The systems are also highly flexible, allowing for easy integration into existing processing lines and the ability to adjust the conveying rate as needed. Furthermore, these systems help to minimize the risk of contamination and damage to the barley, as the grain is enclosed within the conveying line, protecting it from dust, moisture, and other environmental factors. The reduced labor costs and increased operational efficiency are additional benefits that contribute to the overall cost-effectiveness of using pneumatic conveying systems in barley processing.

Ensuring Safety and Compliance in Barley Pneumatic Conveying
When designing and operating a barley pneumatic conveying system, safety is a top priority. The systems are engineered to comply with industry standards and regulations, ensuring that they meet the necessary safety requirements for handling bulk materials. Features such as pressure relief valves, dust explosion-proof designs, and proper ventilation systems are incorporated to prevent accidents and protect personnel. Regular maintenance and inspections are also essential to ensure that the system operates safely and efficiently over its lifespan. HeadPowder Engineering adheres to strict safety protocols in the design and manufacturing of their systems, providing clients with peace of mind that their operations are both safe and compliant.