

What is a Magnesia Pneumatic Conveying System? What is its Design Principle?
Magnesia, a critical component in refractory materials, often requires efficient and reliable transport during production and processing. The magnesia pneumatic conveying system is a specialized equipment designed to handle magnesia powder and related materials using an air-based transport mechanism. This system is essential for industries like refractory manufacturing, where the quality and consistency of material handling directly impact the final product's performance. Understanding the system's components and design principles is crucial for optimizing material transport processes and ensuring operational efficiency.

Components of a Magnesia Pneumatic Conveying System
The magnesia pneumatic conveying system comprises several key components that work together to achieve effective material transport. These components include the material hopper, which stores the magnesia powder; the feeder, which controls the material flow rate; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying line, which transports the material from the hopper to the destination; and the receiver or discharge hopper, where the material is collected. Each component plays a vital role in maintaining the system's performance and ensuring the safe and efficient transport of magnesia.

Design Principles of the Magnesia Pneumatic Conveying System
The design of a magnesia pneumatic conveying system is based on several fundamental principles to ensure optimal performance and material integrity. The first principle is the selection of appropriate air velocity, which must be sufficient to entrain the magnesia particles but low enough to prevent excessive wear on system components. The second principle involves the use of suitable conveying line diameter and length, as these factors directly affect the pressure drop and energy consumption of the system. Additionally, the system design considers the particle size and density of the magnesia, as these properties influence air requirements and overall system efficiency. The design also incorporates air filtration and separation features to prevent material buildup and maintain system cleanliness. These principles are carefully balanced to achieve a reliable and cost-effective magnesia conveying solution.
Applications and Benefits of Magnesia Pneumatic Conveying Systems
Magnesia pneumatic conveying systems are widely utilized in various industrial applications, particularly in the refractory industry. They are employed to transport magnesia powder from storage silos to processing equipment, such as mixers and kilns, with minimal human intervention. The benefits of using this system include improved material handling efficiency, reduced labor costs, and enhanced safety by minimizing direct contact with the material. Additionally, the system helps maintain the purity of the magnesia by preventing contamination from external sources. The ability to transport material over long distances without mechanical conveyors also makes it a versatile solution for different plant layouts. Overall, the magnesia pneumatic conveying system offers significant advantages in operational efficiency and material quality control.
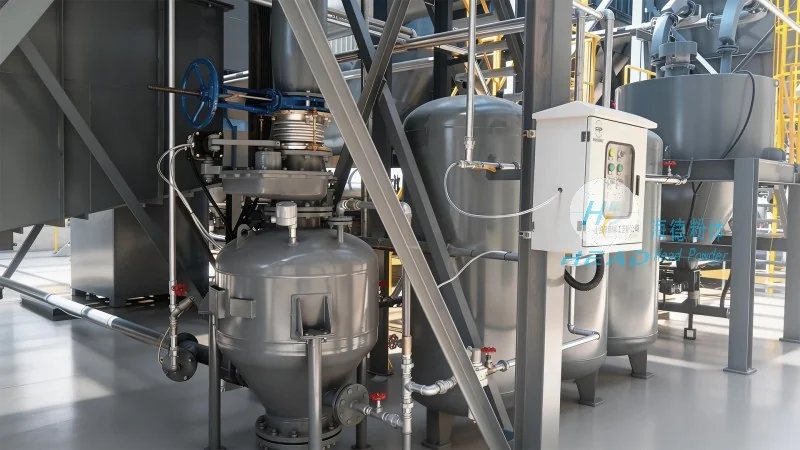
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including magnesia pneumatic conveying equipment. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner in the refractory and material handling sectors. The company specializes in designing and manufacturing customized pneumatic conveying systems tailored to client-specific needs. Its products are recognized for their durability, efficiency, and compliance with industry standards. By leveraging advanced engineering and manufacturing capabilities, HeadPowder ensures that its magnesia pneumatic conveying systems meet high-quality and performance expectations. The company's commitment to innovation and customer satisfaction has made it a preferred choice for businesses seeking reliable material handling solutions.