

Working Principle and Features of Cement Fly Ash Pneumatic Conveying System Equipment
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. The company's expertise lies in developing efficient solutions for transporting bulk materials such as cement and fly ash, which are critical components in construction and industrial applications. This article provides an in-depth look at the working principle and key features of their cement fly ash pneumatic conveying system equipment, highlighting how it addresses the challenges of material handling in modern production environments.
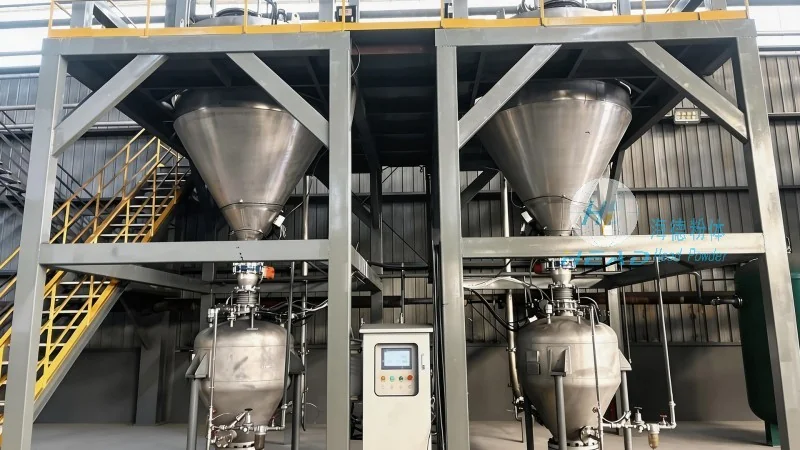
Working Principle of the Pneumatic Conveying System
The cement fly ash pneumatic conveying system operates on the principle of air-based material transport. At its core, the system uses a combination of positive and negative pressure to move bulk materials through a network of pipes. The process begins with the material being fed into a hopper or silo, where it is then drawn into a venturi or a rotary airlock. The air, often supplied by a high-pressure blower or a vacuum pump, creates a flow that propels the material through the pipeline. The system is designed to maintain consistent air pressure and flow rates, ensuring that the material is transported smoothly without blockages or degradation. Key components include the air compressor, material feeders, conveying pipes, and control valves, all of which work in tandem to achieve efficient and reliable material transfer. The system's ability to handle fine powders like fly ash and cement is particularly noteworthy, as it prevents dust accumulation and maintains material integrity throughout the process.

Key Features and Advantages
HeadPowder's cement fly ash pneumatic conveying system offers several distinct advantages that make it an ideal choice for industrial applications. One of the primary features is its high efficiency in material transport, with the ability to move large volumes of material over long distances with minimal energy consumption. The system is also highly flexible, allowing for easy integration into existing production lines and adaptability to different material types and processing requirements. Another notable feature is its low maintenance requirements, thanks to the use of durable materials and advanced sealing technologies that reduce wear and tear. The system's design also prioritizes safety and environmental compliance, with features such as dust collection and air filtration to minimize emissions and protect the working environment. Additionally, the system is equipped with advanced control systems that allow for real-time monitoring and adjustment of parameters, ensuring optimal performance and reducing downtime. These features collectively contribute to improved productivity, reduced operational costs, and enhanced safety in material handling operations.

Performance and Reliability
The performance of the cement fly ash pneumatic conveying system is characterized by its reliability and consistent operation. The system is engineered to handle the specific challenges of transporting cement and fly ash, such as their fine particle size and tendency to agglomerate. The use of positive pressure in the conveying process helps to prevent material buildup and ensures smooth flow through the pipes. The system's control mechanisms, including pressure sensors and flow meters, provide continuous monitoring of key parameters, allowing operators to quickly identify and address any issues that may arise. This proactive approach to maintenance and operation helps to minimize downtime and maximize the system's uptime. Furthermore, the system's design incorporates redundancy in critical components, such as the air compressor and material feeders, to ensure that the system remains operational even in the event of a component failure. This level of reliability is essential for maintaining production continuity in industrial settings where material supply is critical.

Conclusion
HeadPowder's cement fly ash pneumatic conveying system represents a sophisticated solution for efficient material handling in the cement and industrial sectors. By leveraging advanced pneumatic technology and robust engineering, the system offers superior performance, reliability, and flexibility. The working principle, which combines positive and negative pressure with precise control of air flow, ensures that cement and fly ash are transported safely and efficiently. Key features such as high efficiency, low maintenance, and environmental compliance make this system a preferred choice for companies seeking to optimize their material handling processes. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of the industry. The company's commitment to quality and customer satisfaction is reflected in the durability and effectiveness of their pneumatic conveying systems, which are designed to deliver long-term value and operational excellence.