

What is a Heavy Powder Material Conveying System Equipment? What Are Its Design Principles?
Heavy powder material conveying systems are essential in various industrial applications, designed to transport bulk powders efficiently and safely. This article explores the fundamental aspects of such equipment, focusing on its design principles and operational capabilities.
Understanding Heavy Powder Material Conveying Systems
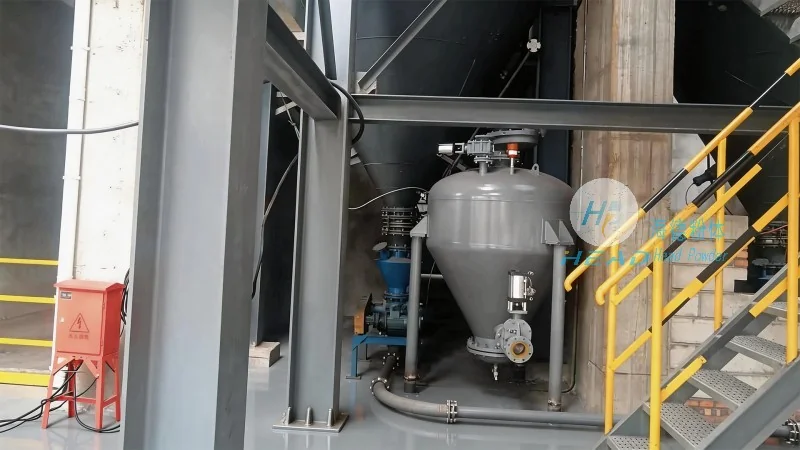
Heavy powder material conveying systems are engineered to handle large volumes of powders, such as cement, flour, or chemical powders, with precision and reliability. These systems are critical in industries like construction, food processing, and pharmaceuticals, where consistent material flow is paramount. The primary goal of these systems is to ensure that powders are transported from one location to another without degradation, contamination, or loss. This is achieved through a combination of mechanical components and intelligent control systems.
Key Components and Design Principles
The design of a heavy powder material conveying system involves several key components, each playing a crucial role in the overall functionality. The core components typically include a feeding mechanism, a conveying device (like a screw or pneumatic system), a control system, and a discharge unit. The feeding mechanism ensures that the powder is introduced into the system at a controlled rate, preventing overloading or blockages. The conveying device then transports the powder through the system, using either mechanical force (e.g., screw conveyors) or pneumatic pressure (e.g., air slides). The control system monitors and adjusts the operation of the components to maintain optimal performance, while the discharge unit safely releases the powder at the destination.

One of the critical design principles is the prevention of material degradation. This is achieved by minimizing friction, impact, and exposure to air, which can cause clumping or degradation of the powder. For example, some systems use flexible hoses or enclosed tubes to reduce friction and prevent contamination. Another key principle is the ability to handle varying powder characteristics, such as different particle sizes, densities, and flowability. This requires adjustable components, such as variable-speed motors or adjustable screw pitch, to accommodate different materials.
Operational Efficiency and Maintenance
Efficient operation of heavy powder material conveying systems is achieved through careful design and regular maintenance. The systems are designed to minimize energy consumption while maximizing throughput. This is often accomplished by using energy-efficient motors and optimizing the conveying path to reduce resistance. Regular maintenance is essential to ensure the longevity and reliability of the equipment. This includes cleaning the conveying lines, inspecting components for wear and tear, and replacing parts as needed. Proper maintenance not only extends the life of the system but also ensures consistent performance and reduces downtime.

Applications and Industry Impact
Heavy powder material conveying systems are widely used across various industries due to their versatility and efficiency. In the construction industry, they are used to transport cement and other building materials to job sites. In the food industry, they are used to transport flour, sugar, and other ingredients to processing facilities. In the pharmaceutical industry, they are used to transport raw materials and finished products with high precision and hygiene. The impact of these systems on industrial operations is significant, as they improve productivity, reduce labor costs, and enhance safety by minimizing manual handling of powders.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design and production of heavy powder material conveying systems. With a focus on innovation and quality, the company has developed advanced solutions tailored to the specific needs of various industries. HeadPowder's systems are known for their durability, efficiency, and reliability, making them a trusted choice for businesses worldwide. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research center. HeadPowder is committed to providing high-quality equipment that meets the evolving demands of the industry, ensuring that its customers can operate their facilities with confidence and efficiency.